


Twin-Screw Extruder Setup for Masterbatch Production
Masterbatch production demands extremely high standards for dispersion and color uniformity, making the twin-screw extruder the core piece of production equipment. Issues such as batch-to-batch color variation, rough granules, poor dispersion, and black specks or impurities often stem not from raw material formulations, but from improper equipment setup or mismatched operating parameters. Drawing on years of experience in commissioning masterbatch production lines, Benk Machinery has compiled standardized commissioning guidelines for twin-screw extruders, suitable for the mass production of black, white, colored, and functional masterbatches.
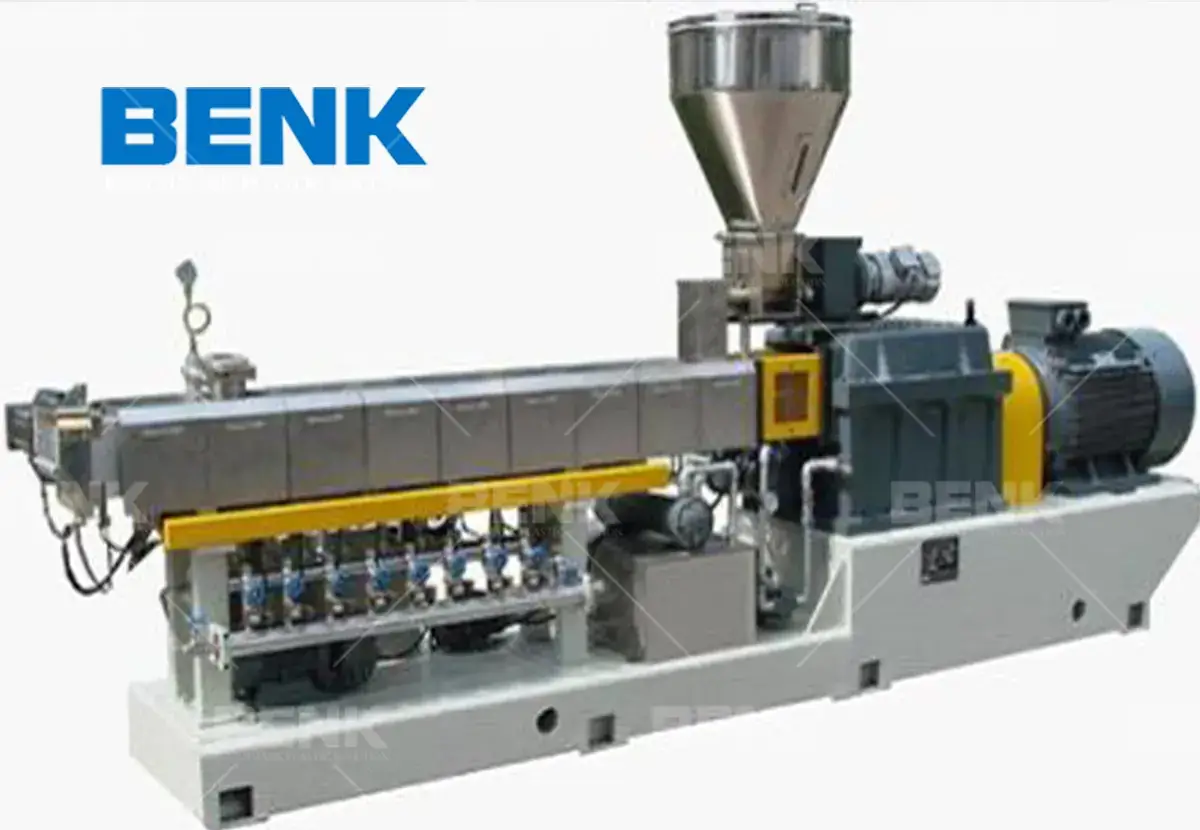
Pre-startup Commissioning and Checks
1. Equipment Status Verification
Before startup, inspect the cleanliness of the screws and barrels to ensure no residual old material or burnt residue affects the color of the new batch. Additionally, check barrel seals, the clarity of vent ports, and the stability of the feeding system to prevent issues such as material leakage, accumulation, or poor venting, thereby laying the foundation for stable production.
2. Screw Configuration Confirmation
Masterbatch production requires a screw configuration designed for high dispersion to ensure pigments and resins blend thoroughly. Adjust the arrangement of kneading blocks based on pigment concentration: increase kneading units for high-concentration masterbatches, and reduce high-shear structures for low-concentration ones to prevent material overheating, decomposition, or discoloration.

Commissioning Standards for Core Process Parameters
1. Zonal Temperature Commissioning
Rapid melting at high temperatures is strictly prohibited during masterbatch extrusion; instead, a zonal gradient heating mode should be used. Maintain a lower temperature in the feed section to prevent material bridging, moderately increase the temperature in the plasticizing section to ensure pigment dispersion, and strictly control the die head temperature to avoid yellowing or graying caused by excessive heat, or uneven dispersion and dry, brittle granules caused by insufficient heat.
2. Matching Screw Speed and Feeding Rate
Adhere to the principle of “low speed with high mixing, and uniform feeding.” Screw speed should not be excessively high to avoid material burning due to shear-induced heat. Precisely match the feeding rate with the screw speed to ensure a stable material fill rate within the barrel, preventing fluctuations that could lead to batch-to-batch color variation or inconsistent granule sizes.
Commissioning the Venting and Pelletizing Systems
Masterbatch production requires unobstructed venting to promptly remove internal moisture and volatiles, thereby preventing defects such as bubbles or voids in the pellets. Simultaneously, calibrating the cutter speed and blade clearance ensures uniform pelletization without fines or long strands. Benk Machinery’s twin-screw extrusion lines feature optimized venting and mixing configurations specifically for masterbatch production, significantly simplifying commissioning and ensuring consistent product quality.
Conclusion
The core of masterbatch extrusion commissioning lies in thorough cleaning, proper screw configuration, balanced temperature and speed settings, and effective venting. Strictly adhering to standardized commissioning procedures can effectively resolve common issues such as color deviation, poor dispersion, and impurities. Benk Machinery offers specialized masterbatch extrusion equipment, on-site commissioning guidance, and process optimization services to help enterprises achieve stable mass production.

FAQ
Q1: What commissioning issues cause significant color deviation in masterbatches?
A: Unstable screw speed or temperature, uneven feeding, or poor screw mixing performance.
Q2: How can I improve rough masterbatch pellets?
A: Optimize the screw’s shear configuration, fine-tune the plasticizing temperature, and stabilize the feed rate.
Q3: Should screw speed be increased for high-concentration masterbatches?
A: No; prioritize optimizing the mixing configuration instead, as excessive speed can cause thermal decomposition of the material.
Q4: Does a clogged vent affect masterbatch quality?
A: Yes; it can lead to bubbles or voids in the pellets, resulting in substandard finished products.
Q5: Can Benk Machinery provide customized masterbatch extrusion equipment?
A: Yes; we offer complete twin-screw extrusion lines and process solutions tailored for various types of masterbatches.
Why Choose Benk Machinery?
From individual machines to complete production lines, Benk Machinery provides reliable and customized plastic processing solutions. Since 2012, we have focused on plastic extrusion, nergy-saving plastic recycling machine, and automated compounding centralized feeding systems, helping customers build efficient and cost-effective production facilities.

- Complete Extrusion Solutions: Professional expertise in plastic pipe, profile, sheet, plate and board extrusion lines.
- Customized Project Solutions: Equipment and production lines can be configured according to your materials, products, capacity and factory requirements.
- Stable & Cost-Effective Equipment: Reliable machine performance, efficient production and optimized energy consumption help reduce operating costs.
- Professional Service: From technical consultation and production to installation, commissioning and after-sales support, our team provides complete project assistance.
Contact Benk Machinery:
PPlanning to upgrade your factory? Contact Benk Machinery for a customized project solution.
- Email: [email protected]
- Tel / WhatsApp: +8615950962426

